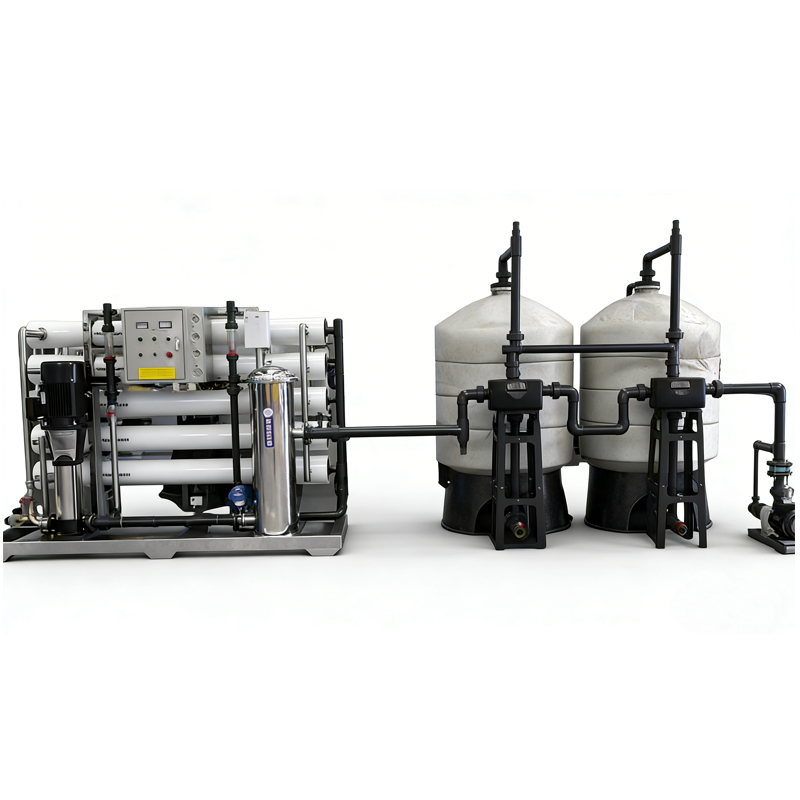
Our Industrial Water Treatment System is engineered for food processing, beverage production, pharmaceutical, and other water-sensitive industries, delivering reliable, high-purity water solutions to ensure product safety and consistency.
Key Features:
- Customizable Solutions: Tailored processes including Reverse Osmosis (RO), Ultrafiltration (UF), and Water Softening are available to match your raw water quality (groundwater, tap water, surface water) and production requirements.
- Efficient & Stable Purification: Multi-stage filtration effectively removes impurities, heavy metals, microorganisms, and residual chlorine, producing water that meets international food-grade standards.
- Smart Operation: Equipped with a PLC automatic control system for auto-backwashing, real-time water quality monitoring, and fault alerts, minimizing manual intervention and operational costs.
- Durable & Hygienic: Constructed from food-grade stainless steel (304/316) for corrosion resistance and easy cleaning. Modular filter design simplifies maintenance and replacement.
- Food Industry Ready: Optimized for food processing lines (nut roasting, beverage filling, meat processing, etc.), complying with strict hygiene and safety regulations.
Technical Highlights:
- Capacity: Customizable from 0.5 to 50 tons per hour
- Core Technology: RO / UF / Softening (optional)
- Control: Fully automatic / semi-automatic
- Material: Food-grade stainless steel
Reviews
There are no reviews yet.